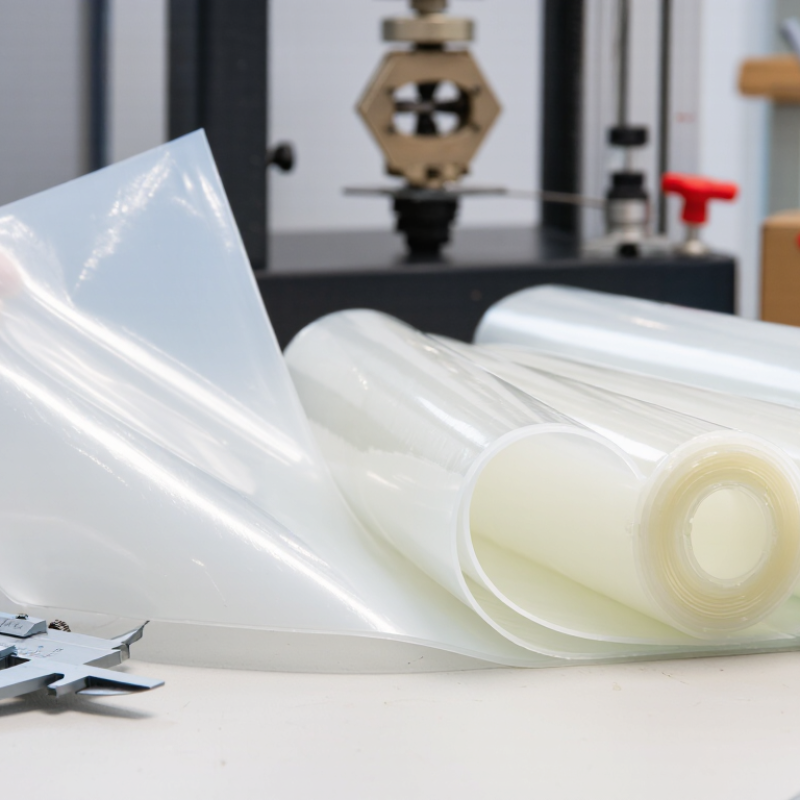
Choosing Durable Pvc Urine Bag Film requires more than checking thickness or price. The film must remain flexible, leak-resistant, weldable, and stable during storage and clinical handling. Grand View Research’s PVC market analysis identifies medical applications as a major performance-driven segment, while MarketsandMarkets reports continued demand for medical plastics with improved safety and processing reliability. These findings support a practical question: can the film survive real use, not just laboratory inspection?
Dr. George Wypych, author of the PVC Handbook, states, “PVC performance depends on formulation, processing, and service conditions.” This principle is central to selecting Durable Pvc Urine Bag Film. A suitable grade should demonstrate controlled plasticizer migration, consistent tensile strength, and reliable heat-sealing behavior. It should also support biocompatibility evaluation under ISO 10993 and align with applicable urine collection device requirements, including ISO 8669 where relevant. Look closely.
A clear film may reveal gel particles, uneven thickness, or weak seal zones before production begins. Flexing tests should imitate transport, bedside movement, and repeated handling. Chemical compatibility testing matters too, especially when disinfectants or cleaning residues contact the outer surface. Yet no material choice is perfect. A thicker film can improve puncture resistance, but it may reduce softness and increase manufacturing waste. Supplier certificates help, but independent verification remains necessary. This guide examines the evidence, testing methods, and design trade-offs behind a safer, more durable selection.
Medical-grade PVC film must begin with a documented ISO 10993 biocompatibility plan. ISO 10993-1:2018 requires evaluation based on contact type, body contact duration, and biological risk. A urine bag may contact urine continuously and touch skin during handling. The final film, not only the resin, needs assessment. Plasticizers, pigments, adhesives, printing ink, and processing residues can change the result.
Duration matters. The FDA’s 2023 guidance describes limited contact as 24 hours or less, prolonged contact as over 24 hours to 30 days, and permanent contact as beyond 30 days. Urine bag film commonly falls within prolonged exposure during use. Testing may therefore include cytotoxicity under ISO 10993-5, irritation or sensitization under relevant ISO 10993 methods, and chemical characterization under ISO 10993-18. Extractables and leachables deserve close attention.
A practical review checks tear resistance, seam strength, puncture performance, and flexibility after sterilization. ISO 10993-23 can support irritation assessment, but test conditions must reflect real use. A film that passes before sterilization may perform differently afterward. This is where supplier data can mislead. Ask for lot-specific certificates, formulation disclosure, and aging evidence. I would also compare samples after folding, hanging, and simulated filling. Perfect compliance on paper is not enough. Real handling can reveal weak seals, odor, or unexpected brittleness.
How to Choose Durable PVC Urine Bag Film for Medical Use?
Durability targets should begin with measurable film performance. Set a minimum tensile strength of 15 MPa for the selected PVC film. This value helps the bag resist pulling during filling, handling, and transport. Test specimens in both machine and transverse directions. Film strength can vary noticeably between them. Check elongation too, because a strong film may still split when stretched around a connector.
Tear resistance needs a defined method, not a visual guess. ASTM D624 tear testing can provide useful data for flexible polymer materials. However, laboratories should confirm its suitability for the specific PVC formulation. The method was developed mainly for rubber and thermoplastic elastomers. Record the die type, specimen thickness, conditioning temperature, and test speed. Small differences can change the result. Inspect the tear path carefully. A smooth, steady tear differs from a sudden split near a seal.
A practical qualification plan includes virgin film, printed film, and heat-sealed samples. Test several production lots, not only one attractive sample. I once treated a high tensile result as proof of reliability; that was too simple. The film later showed weak corners after aging. Recheck samples after heat, humidity, and simulated storage exposure. Keep raw data, equipment calibration records, and acceptance limits with the batch file. A 15 MPa result is only a starting point. Bag geometry, weld quality, and handling conditions still influence real-world performance.
The film should achieve a minimum tensile strength of 15 MPa. Tear resistance should be evaluated using ASTM D624; the 40 kN/m value shown is an example internal engineering target, because ASTM D624 defines the test method rather than a universal pass/fail limit.
Acceptance values should be confirmed through laboratory testing of the selected PVC formulation, film thickness, weld design, sterilization process, and storage conditions.
Durable PVC urine bag film needs more than suitable thickness. Puncture resistance should be measured under controlled, repeatable conditions. ASTM F1306 evaluates slow-rate penetration resistance in flexible films and laminates. A probe presses through the film at a defined speed. The recorded peak force reveals how much stress the material can withstand. Penetration energy also helps compare different formulations. Higher values usually indicate better resistance, but they do not guarantee reliable bags.
Test specimens from the film center, edges, and welded areas. Weakness may appear near seals, where heat and pressure change the PVC structure. Condition samples at realistic temperatures and humidity levels before testing. Cold film can become stiff and crack during handling. Warm film may soften and show different puncture behavior. Record thickness, conditioning time, probe details, and failure appearance. Small details matter.
ASTM F1306 is not a complete flex-cracking test. For practical evaluation, flex the film repeatedly before penetration testing. Inspect whitening, pinholes, and surface splits under magnification. Then compare puncture results before and after flexing. A large performance drop deserves investigation. I would not rely on one attractive test value. Film variability, storage age, plasticizer movement, and manufacturing seams can change the result. One overlooked corner may matter more than a perfect laboratory sheet.
How to Choose Durable PVC Urine Bag Film for Medical Use?
A durable PVC urine bag film needs reliable seals, not only strong material thickness. In practical production, ASTM F88/F88M seal-strength testing helps measure opening force after sealing. Set an acceptance target of at least 1.0 N/mm. Test samples from the top, middle, and bottom seal areas. Variations can reveal uneven heat, pressure, or dwell time. The test is destructive. That is useful.
Inspect the failure pattern, not only the recorded number. A clean, consistent peel may indicate a controlled process. Film tearing, channel leaks, or weak corners need investigation. Test conditioned samples after storage, handling, and suitable aging exposure. A seal can pass immediately but weaken later. I have found that apparently minor wrinkles often create serious leakage paths. This detail is easy to overlook.
Tips: Use multiple specimens from different production lots. Record sealing temperature, pressure, and dwell time beside every result. Confirm the laboratory’s calibration and test speed. Do not treat 1.0 N/mm as the only durability measure. Flexing, puncture resistance, weld geometry, and connector attachment also matter. If results sit close to the limit, review the process instead of accepting them too quickly. Higher strength is not always better when the film becomes brittle or difficult to open safely.
| Selection Dimension | Recommended Requirement or Reference Value | Verification Method | Why It Matters for a Urine Bag |
|---|---|---|---|
| Film Construction and Material Control | |||
| Film polymer | Flexible medical-grade polyvinyl chloride (PVC) suitable for fluid-contact applications. | Review material specification, formulation declaration, and incoming inspection records. | Supports consistent flexibility, weldability, and compatibility with the intended medical application. |
| Nominal film thickness | 0.25–0.35 mm, with a controlled tolerance defined in the purchasing specification. | Measure at multiple locations using a calibrated thickness gauge; avoid sealed edges and printed areas. | Thicker film generally improves puncture and handling resistance, but excessive thickness can reduce flexibility and increase sealing energy. |
| Thickness uniformity | Target variation: no more than ±10% from the nominal thickness within a roll or lot. | Take measurements across the web width and along the roll length using a documented sampling plan. | Uniform thickness helps maintain consistent heat transfer, seal formation, and mechanical performance. |
| Plasticizer and additive disclosure | Full formulation disclosure to the applicable regulatory assessor, including plasticizer type, stabilizers, pigments, and processing aids. | Supplier declaration supported by chemical documentation and, where required, extractables or biocompatibility evaluation. | Plasticizer migration, odor, discoloration, or incompatibility can affect safety and product durability. |
| Visual appearance | No pinholes, gels, cracks, foreign particles, delamination, or visible streaks in the functional area. | 100% visual inspection under controlled illumination, supplemented by leak testing. | Surface defects can become leakage paths or stress-concentration points during use. |
| Seal Strength and Leak-Resistance Verification | |||
| Seal strength acceptance criterion | Minimum ≥1.0 N/mm of seal width. This equals ≥25 N per 25 mm of seal width. | ASTM F88/F88M seal-strength testing. Report the force, specimen width, seal mode, failure mode, and test conditions. | Provides a measurable minimum strength for welded seams and reduces the risk of seal opening during filling, transport, or handling. |
| Recommended ASTM F88/F88M specimen | Specimen width: 25 ± 1 mm; test at least five specimens per production lot or according to the validated sampling plan. | Cut specimens perpendicular to the seal and avoid corners, tubing junctions, and visibly defective areas unless those locations are being evaluated separately. | A consistent specimen geometry makes results comparable between lots and process settings. |
| Test conditioning | Condition specimens for at least 24 hours at 23 ± 2°C and 50 ± 5% relative humidity, unless the validated procedure specifies otherwise. | Record conditioning time, temperature, humidity, seal age, and equipment identification. | Temperature and humidity can change PVC flexibility and produce misleading seal-strength results. |
| Test speed and jaw separation | Use a validated constant crosshead speed, such as 200 mm/min, and apply the same speed to comparative testing. | ASTM F88/F88M-compatible tensile tester with calibrated load cell; document the selected test method and speed. | Test speed affects measured peak force and must remain consistent for meaningful trend analysis. |
| Seal failure mode | Prefer cohesive film failure, controlled yielding, or peel failure above the minimum strength; reject channel leaks, unsealed areas, and brittle tearing. | Record the failure mode for every specimen, not only the numerical peak force. | A high force value alone may not identify a continuous leakage path or a localized weak point. |
| Seal width | Use a continuous seal width appropriate to the bag design; a nominal 3–6 mm welded area is common for many flexible medical-bag constructions, subject to design validation. | Measure the actual welded width at several locations and verify the complete perimeter or seam design. | Adequate seal width distributes load and helps compensate for normal variation in film thickness and process temperature. |
| Seal process window | Establish validated ranges for temperature, pressure, dwell time, and cooling time rather than relying on a single setting. | Run process-window studies and confirm that all tested settings maintain at least 1.0 N/mm with acceptable failure modes. | A process window improves robustness against changes in equipment, line speed, ambient conditions, and film lots. |
| Leak test after sealing | No visible leakage or pressure decay exceeding the validated product limit. | Use a validated air-pressure decay, immersion, vacuum, or dye-penetration method appropriate to the finished bag. | Seal-strength testing measures mechanical resistance, while leak testing confirms functional fluid containment. |
| Mechanical and Functional Performance | |||
| Tensile strength | Set a project-specific minimum in both machine and transverse directions; a practical development target for flexible PVC film is approximately 15–25 MPa, subject to formulation and thickness. | Test according to ISO 527-3 or another validated thin-film tensile method, reporting direction, specimen type, speed, and conditioning. | Helps prevent tearing during bag filling, suspension, transport, and connection to drainage tubing. |
| Elongation at break | Define a minimum based on the bag geometry; flexible PVC constructions commonly require high elongation to tolerate bending and handling. | Measure with the same tensile method used for tensile strength and report machine and transverse directions separately. | Insufficient elongation can cause cracking or tearing when the filled bag is flexed or dropped. |
| Puncture and tear resistance | Use internally established minimum values based on bag volume, wall design, packaging, and transport hazards. | Evaluate with validated puncture and tear procedures, such as ISO 6383-2 for tear propagation where applicable. | Urine bags may contact bed rails, clamps, packaging edges, and other objects that can initiate a tear. |
| Flex-crack resistance | No functional cracks or leakage after the validated repeated-flexing cycle. | Perform a product-specific flexing test on film and finished bags, followed by visual inspection and leak testing. | Repeated folding around tubing connections or during storage can weaken the film even when initial strength is acceptable. |
| Tube and port attachment | Attachment seals must meet the same or a separately validated mechanical and leak-resistance requirement as the main bag seam. | Conduct tensile pull, torque or bend evaluation, and leak testing on representative finished assemblies. | Ports and tubing junctions are common stress concentrations and should not be qualified only by flat-film seam testing. |
| Transparency and readability | Film should permit visual monitoring of liquid level, color, and particulate matter, with haze controlled to the product requirement. | Use a validated haze or optical inspection method and inspect filled finished bags under intended-use lighting. | Clear visual observation supports monitoring of volume and unusual contents during clinical use. |
| Lot Release and Documentation | |||
| Lot traceability | Each film lot should have traceable resin/additive records, manufacturing date, roll identification, thickness, and test results. | Review the certificate of analysis and match roll labels to production and inspection records. | Traceability enables containment and investigation if a seal or leakage trend is detected. |
| Routine seal-strength testing | Test start-up samples, periodic production samples, and samples after material, tooling, or process changes. | Use a documented sampling plan with a minimum acceptance value of ≥1.0 N/mm and defined retest rules. | Routine testing verifies that the validated sealing process remains in control throughout production. |
| Finished-bag visual and leak inspection | No open seams, pinholes, wrinkles crossing seals, incomplete welds, or visible contamination. | Inspect 100% of finished bags where feasible, followed by the validated leak test required by the product specification. | Detects defects that a small number of flat-seal tensile specimens may not represent. |
| Change control | Requalify film and seals after changes to PVC formulation, plasticizer, thickness, supplier, sealing equipment, tooling, or process parameters. | Repeat applicable seal-strength, leak, mechanical, and compatibility evaluations using documented change-control procedures. | Small material or process changes can alter sealing behavior, flexibility, extractables, and long-term durability. |
| Overall purchasing decision | Accept only when the film meets the approved medical-material requirements, the seal strength is ≥1.0 N/mm, failure modes are acceptable, and finished bags pass leak testing. | Review the complete qualification package rather than relying on thickness or seal-strength data alone. | Durability is a combination of material consistency, seam performance, attachment integrity, and finished-product leak resistance. |
Durable PVC urine bag film must remain flexible after sterilization, storage, and handling. Start by checking the resin, plasticizer system, film thickness, and heat-seal compatibility. A thicker film is not automatically safer. Weak welds can still cause leakage. The chosen material should be evaluated against the applicable ISO 8669 requirements and the intended urine collection design.
Sterilization stability deserves close attention. Test the film before and after the planned sterilization process. Inspect color, odor, flexibility, tensile strength, and seal quality. Then perform leak testing under the conditions specified by the relevant ISO 8669 test method. Check the complete assembly, including tubing joints, outlet ports, and welded seams. Small channels may appear only after conditioning or repeated handling. A first screening can look reassuring, yet it may miss long-term brittleness. That is an important limitation.
Tips: Request test reports from an independent, competent laboratory. Confirm the ISO 8669 edition and test scope. Use samples from normal production, not specially selected sheets. Compare results after sterilization, aging, folding, and simulated transport. Record failures with photographs and measurable data. Also review whether the film’s softness changes patient comfort or packaging performance. Practical evidence matters more than a confident specification sheet.