How to Choose the Right Dual Energy Inspection System?
Choosing a dual-energy inspection system is not simply a matter of selecting the highest resolution available. It requires a practical match between materials, product flow, operating speed, and inspection objectives. Dual Energy Inspection separates materials according to how they absorb different X-ray energies. That distinction can reveal contrasts that single-energy imaging may overlook.
W. Edwards Deming, a widely respected authority on industrial quality, said, “Without data, you’re just another person with an opinion.” His principle remains useful here. A reliable decision should begin with measurable evidence, not impressive brochures. Request test scans using your actual products, packaging, conveyor speed, and expected material variations. Examine image clarity, false-alarm frequency, software usability, maintenance access, and operator training requirements.
Look closely at real working conditions. Will dense packaging create overlapping images? Will moisture, temperature, or irregular product shapes affect detection? Can the system maintain stable performance during long production shifts? These details often matter more than a specification sheet.
The choice is rarely perfect. A faster system may provide less analytical detail. A more sensitive platform may require additional calibration. Some suppliers may also present limited test samples. That deserves reflection.
A strong evaluation combines engineering judgment, documented trial results, and feedback from experienced operators. It should also consider integration with existing conveyors, inspection records, service support, and future production changes. The right Dual Energy Inspection system is not merely powerful. It is consistent, understandable, maintainable, and suited to the decisions your team must make every day.
Define the Inspection Goals and Operating Environment
Choosing a dual energy inspection system starts with a clear inspection goal. Define what must be detected, measured, or separated. Different materials can overlap in a standard X-ray image. Dual energy analysis may improve recognition, but it cannot correct unclear requirements.
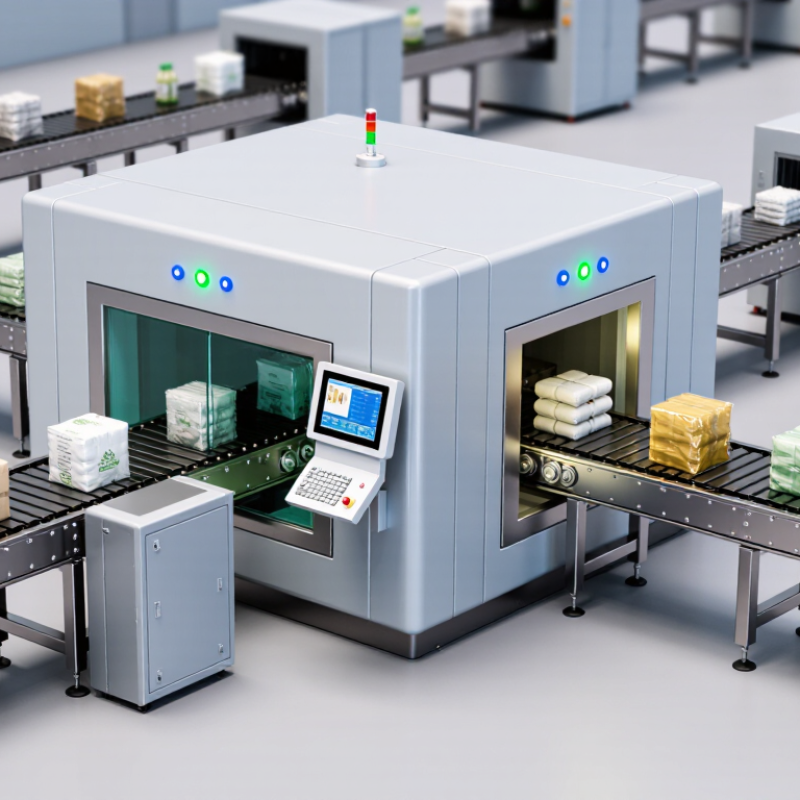
Consider product size, material density, package shape, and line speed. A system for small sealed parcels may need different settings from one handling large cartons. Record the tunnel opening, conveyor height, ambient temperature, dust level, and vibration. These details affect image stability and maintenance needs.
In practical evaluations, sample testing is essential. Use real products, including difficult items and normal variations. A clean test image can mislead. My own early evaluations sometimes focused too much on detection performance and too little on operator workflow.
Tips:
Test samples during the fastest planned operating speed. Check image quality after warm-up, not only at startup. Ask operators to complete routine tasks without assistance. Review false alarms, cleaning time, calibration steps, and data storage requirements. Leave space around the system for inspection and service access. A compact design may appear efficient, yet poor access can increase downtime. Also, document failed tests honestly. They often reveal packaging changes, unstable positioning, or unsuitable settings. Require clear technical records, training materials, and responsive service procedures before making a final decision.
Compare Dual Energy Technologies and Image Quality
Choosing a dual-energy inspection system starts with image quality, not a headline specification. Dual-energy imaging captures the same object at two energy levels, then compares attenuation differences. This helps separate low-density and high-density materials more clearly. However, sharper images do not always mean better discrimination.
Three common designs deserve comparison: dual-layer detectors, rapid energy switching, and separate X-ray sources. Dual-layer detectors provide stable alignment because both energy signals arrive together. Rapid switching can offer strong contrast, but timing errors may create edge artifacts. Separate sources provide flexible energy control, although calibration becomes more demanding. ASTM F792-17 recommends evaluating security X-ray imaging through measurable factors, including spatial resolution, penetration, contrast sensitivity, and image uniformity. Test these conditions with fine wires, stepped materials, and unevenly packed objects. Look closely at the corners.
Throughput also affects real image quality. ACI World’s 2024 World Airport Traffic Forecast estimated about 9.5 billion airport passengers in 2024. Busy checkpoints require fast scanning without excessive motion blur or repeated scans. Ask vendors for measured results at operating speed, not laboratory speed. Compare false-alarm rates, detector aging, and performance across different object sizes. One overlooked issue is operator fatigue. A technically excellent image can still fail when colors look confusing after hours of viewing. My own assessment would not rely on a single test image. Real-world conditions are messier.
Evaluate Detection Performance for Target Materials
How to Choose the Right Dual Energy Inspection System?
Evaluate Detection Performance for Target Materials
Detection performance should match the materials your operation handles daily. A system may perform well with dense metals but struggle with thin plastics, rubber, or layered food packaging. Define target materials before comparing specifications.
Use representative test samples, not only laboratory objects. Include different thicknesses, shapes, moisture levels, and package positions. A sealed carton can look very different when its contents overlap. Observe how clearly the system separates organic and inorganic materials. Check whether operators can identify small variations without excessive image enhancement.
Measure more than image sharpness. Record detection rates, false alarms, inspection speed, and results across repeated trials. Certified test pieces can support consistent comparisons. Blind testing is useful because familiar samples may influence operator judgment. Review the system under realistic conveyor conditions, including vibration and uneven spacing.
Ask trained users to assess the workflow. Their experience often reveals practical weaknesses that brochures omit. Interfaces, alert timing, and image storage can affect decisions. No system performs perfectly. Material signatures may overlap, and calibration can drift over time. We once treated a strong contrast image as proof of reliable detection; later testing showed that packaging orientation changed the result. That lesson matters. Schedule regular verification, document uncertain cases, and involve qualified technical personnel when setting performance limits.
Assess Throughput, Integration, and Operator Usability
How to Choose the Right Dual Energy Inspection System?
Throughput should be measured at peak load, not from a brochure’s maximum speed. Count trays, images, alarms, and manual diversions per minute. A system that pauses during image analysis can create visible queues quickly. Speed is not enough. SITA’s Baggage IT Insights 2024 reported 6.9 mishandled bags per 1,000 passengers in 2023. This figure shows why inspection equipment must exchange accurate status data with conveyors and baggage systems. Ask for API documentation, event timestamps, failure alerts, and recovery procedures. Then test them under realistic network interruptions.
Integration also includes people. The system should connect with existing screening workflows, access controls, maintenance tools, and audit records. NIST’s Cybersecurity Framework 2.0 supports clear asset ownership, monitoring, and incident response. Those principles are practical for inspection environments. They are not decorative paperwork. Operators need readable images, consistent alarm signals, adjustable displays, and minimal menu depth. IATA’s 2024 Global Passenger Survey found that 70% of travelers supported biometric identification for smoother airport processing. Passenger expectations are rising, but staff still need clear decisions behind every automated prompt.
The screen matters. Operators should complete common tasks with limited training. Test the system after several hours, when attention drops and glare becomes annoying. Measure false alarms, review time, and handoff errors. A perfect laboratory score can mislead. I would also leave room for doubt: newer automation may reduce workload, yet poorly designed interfaces can simply move mistakes elsewhere.
Review Safety, Compliance, Maintenance, and Total Cost
Choosing a dual energy inspection system starts with safety, not image sharpness. The IAEA’s General Safety Requirements Part 3 sets a 1 mSv annual dose limit for public exposure. Ask suppliers for measured dose data, shielding records, and operator training evidence. A glossy demonstration is not enough.
Workload matters too. TSA screened about 858 million passengers in 2023, according to its Annual Report. ACI World forecast roughly 9.5 billion air passengers worldwide in 2024. These figures highlight the need for stable throughput, clear alarms, and dependable software during peak hours. Compliance should cover local radiation rules, electrical standards, cybersecurity, and inspection procedures. Requirements vary by site. That detail is easy to miss.
Maintenance should be judged through real operating costs. Request mean time between failures, spare-parts availability, remote-support limits, calibration intervals, and technician response targets. Compare energy use, training hours, software updates, and disposal costs over the system’s full life. The cheapest quotation may create expensive delays. A perfect detection score is unrealistic, too. Operator fatigue, poor loading, and weak procedures can reduce performance. Review those risks honestly before approving the purchase.
How to Choose the Right Dual Energy Inspection System?
The chart compares three common system profiles across safety, compliance, maintenance, and total cost of ownership. Scores are normalized from 0 to 100, with higher values indicating a stronger procurement position. Safety and compliance should be treated as mandatory requirements, while maintenance and total cost help determine long-term operational value.