China remains a major global manufacturing base for construction fasteners, including stainless steel wood screws. The International Stainless Steel Forum reports that worldwide stainless steel production exceeds 50 million tonnes annually. This scale supports broad material availability, but it also creates quality differences between suppliers.
Choosing the right product requires more than comparing prices. Check the steel grade, thread design, head shape, drive type, coating, and dimensional tolerance. For outdoor timber, 304 stainless steel often provides practical corrosion resistance. Coastal or chemically aggressive environments may require 316 stainless steel. The ISO 3506-1 standard offers recognized guidance on stainless fastener grades and mechanical properties. ASTM specifications can provide additional reference points for North American projects.
Supplier evidence matters.
Ask for mill certificates, batch traceability, salt-spray results, and tensile or torque test records. The International Organization for Standardization emphasizes documented conformity and repeatable testing. A reliable Chinese manufacturer should explain its wire source, cold-forming process, heat treatment, inspection frequency, and packaging method. Product samples should be tested in actual wood, not only examined visually.
Market research from Grand View Research and Mordor Intelligence indicates continuing growth in global fastener demand, driven by construction, furniture, and renovation activity. However, market growth does not guarantee consistent screw performance. A polished catalog can hide weak threads, soft drive recesses, or mixed material grades.
That is the difficult part.
Buyers should compare total cost, not unit price alone. A low-cost screw that snaps during installation can increase labor, waste, and project delays. This guide examines how to choose stainless steel wood screws from China with practical checks, recognized standards, supplier verification, and a willingness to question attractive claims.
Stainless steel grade strongly affects a wood screw’s service life. Grade 304 suits interior furniture, dry framing, and ordinary outdoor projects. It resists moisture well, but salt air can expose its limits. Grade 316 performs better near coasts, swimming pools, and treated timber containing harsh chemicals. Its added molybdenum improves resistance to chloride corrosion. Grade 410 is harder and stronger, yet it offers less corrosion protection than 304 or 316. Grade 201 may reduce cost, but I would use it cautiously in damp environments. Stainless steel is not completely rust-proof.
Tips: Request the steel grade, hardness, and production batch records. Ask for a material test certificate, then compare it with an independent test when the project matters. Check thread sharpness, head seating, and drive torque with real wood samples. A polished surface can look impressive, but it cannot replace correct metallurgy.
In sourcing work, I have seen screws marked “stainless” without clear grade evidence. That creates avoidable uncertainty. Ask Chinese suppliers about cold heading, passivation, and salt-spray results. Also inspect samples after drilling into oak, cedar, or pressure-treated lumber. Some screws resist corrosion but snap during installation. Others drive smoothly but leave staining around the hole. My earlier assumption was simple: a higher grade always solved the problem. It did not. Wood species, moisture, installation speed, and cut-edge exposure all influence performance. Reliable selection combines documents, practical testing, and honest discussion of project conditions.
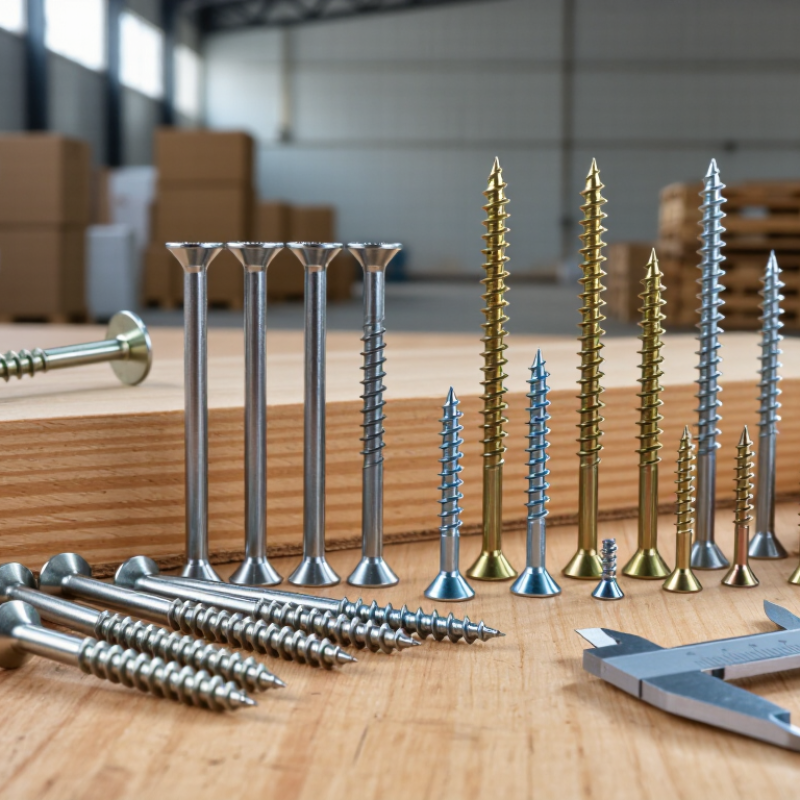
Choosing stainless steel wood screws requires more than checking the diameter and price. In sample inspections, I measure the screw length from the bearing surface to the tip. A 4 × 40 mm screw may suit a light indoor joint, while thicker timber needs greater holding depth. Keep enough embedded length without piercing the opposite face. Small details matter.
Head shape also affects performance. A countersunk head should sit flush in hardwood without splitting the surface. A washer head can spread pressure across softer wood. The drive recess must remain deep and clean after installation. Measure the shank, too. An oversized shank can create excessive resistance and break delicate wood fibers.
Thread design controls grip. Coarse, deep threads usually bite well in softwood and reduce installation time. Finer threads can work better in dense hardwood, especially with a prepared pilot hole. Partial threads pull two boards together, while full threads provide stronger positioning in some assemblies. Sharp points help initial penetration, but they do not replace drilling when the wood is dry or brittle.
I once accepted a screw based only on its bright surface. That was careless. Confirm the stated stainless steel grade through material reports and sample testing. Stainless steel type, thread consistency, and corrosion resistance should match the application. For coastal projects, environmental exposure deserves extra attention. The best dimensions depend on the wood, joint thickness, driver torque, and installation method.
How to Choose Top Stainless Steel Wood Screws from China?
Quality Standards and Manufacturing Checks to Evaluate
A reliable screw starts with verified stainless steel, not a bright surface. Request the material grade, heat number, and mill certificate for every production lot. A2 stainless steel suits many indoor and mild outdoor applications. A4 offers stronger corrosion resistance near saltwater or chemical exposure. Do not accept grade labels alone.
Check whether the factory follows relevant standards, such as ISO 3506, ASTM F593, or applicable timber-screw requirements. Confirm the actual dimensions against approved drawings. Measure head diameter, shank length, thread pitch, and point shape. Inspect thread consistency with calibrated gauges. Test hardness, tensile strength, and torsional performance through an independent laboratory when risk is high. Small samples can reveal large problems.
Manufacturing control matters daily. Ask for incoming wire inspection, controlled forming, heat treatment records, passivation details, and final sorting procedures. A useful audit should trace one carton back to its raw material lot. Inspect packaging for mixed sizes or missing labels. Salt-spray results may help, but they cannot replace alloy verification or field testing. A polished screw can still fail early. That lesson is easy to miss. I would also test installation torque in the target wood, because laboratory results may not reflect stripped heads, split timber, or inconsistent driver settings. Keep retained samples and compare them during repeat orders. Reliability grows from records, repeat checks, and honest discussion of defects.
| Evaluation Dimension | Recommended Requirement | Practical Acceptance Criteria | Manufacturing Check or Test | Required Evidence | Common Warning Signs |
|---|---|---|---|---|---|
| Stainless Steel Grade | Specify the required grade before quotation, normally A2 stainless steel for general outdoor use and A4 stainless steel for higher chloride or coastal exposure. | The material designation on the purchase order, product drawing, packaging, and test report must match. | Perform positive material identification using X-ray fluorescence (XRF). Use optical emission spectroscopy when carbon content or closer grade discrimination is necessary. | Material test certificate showing the standard, grade, heat or batch number, and chemical composition. | The supplier describes the product only as “stainless” without identifying the grade or material standard. |
| Mechanical Property Class | For ISO 3506-1 property classes, A2-70 and A4-70 indicate a minimum nominal tensile strength of 700 MPa for applicable fasteners. | The ordered property class and required mechanical values are stated clearly; results meet the applicable standard or approved product specification. | Carry out tensile testing on representative samples when the screw design and test setup permit. For small wood screws, use a product-specific strength or driving specification. | Laboratory tensile or mechanical test report linked to the production lot. | A high strength claim is made without a property class, test method, or lot traceability. |
| Chemical Composition | Composition must conform to the selected stainless steel grade and the applicable material standard. | Measured alloying elements are within the specified grade limits. The heat number is consistent across the raw material and finished-goods records. | Review the mill certificate and verify selected samples by XRF or another suitable laboratory method. | Original or traceable mill certificate, incoming inspection record, and sample identification. | The certificate has no heat number, shows inconsistent chemistry, or cannot be connected to the finished batch. |
| Dimensions and Geometry | Control overall length, nominal diameter, head diameter, head height, point geometry, thread length, and recess dimensions according to the approved drawing. | All critical dimensions fall within the drawing tolerances. Non-critical tolerances are agreed in writing before production. | Use calibrated digital calipers, micrometers, optical measuring equipment, profile gauges, and go/no-go gauges where appropriate. | Dimensional inspection report with sample size, actual readings, instrument identification, and calibration status. | The supplier relies only on a visual comparison or provides measurements without tolerances. |
| Thread Form and Pitch | Use a thread profile suitable for wood or engineered wood. Confirm the nominal diameter, pitch, thread angle, and partial or full-thread design required for the application. | Threads are continuous, clean, and free from rolled-over crests, severe burrs, cracks, and blocked areas. | Inspect thread profile under magnification and verify pitch and diameter with gauges or optical measurement. Conduct installation trials in the specified substrate. | Thread inspection records and installation-test results using the agreed pilot-hole and substrate conditions. | The screw requires excessive driving force, strips the wood, or shows inconsistent thread depth between samples. |
| Head and Drive Recess | Specify head style, countersink angle where applicable, recess type, recess size, and required driver compatibility. | The bit seats fully and remains engaged without cam-out under the agreed installation torque. | Check head dimensions with gauges and perform repeated driving tests using the specified bit, speed, torque, and substrate. | Drive-recess inspection report and photographs or records from functional driving tests. | The bit wobbles, the recess deforms easily, or the head is not flush after installation. |
| Surface Condition | Surface should be clean, uniform, and free from scale, oil residue, sharp burrs, cracks, laps, and damaging tool marks. | No defects are visible at the agreed inspection distance. The point and cutting features remain sharp and consistent. | Conduct 100% visual inspection or an agreed sampling inspection under suitable lighting. Use magnification for critical features. | Visual inspection standard, defect classification, photographs, and sampling records. | Black stains, embedded metallic particles, rust spots, rough heads, or mixed surface appearances are present. |
| Corrosion Resistance | Select A2 or A4 according to the environment. Do not use a salt-spray result alone to predict service life in a real installation. | The alloy grade, passivation or cleaning process, packaging, and any agreed corrosion test all meet the purchase specification. | Inspect after cleaning and passivation. If required, use a controlled salt-spray test according to ASTM B117 or another agreed method, with the exposure duration and failure criteria defined in advance. | Process record, corrosion-test report, and clearly defined acceptance criteria. | A supplier quotes “hours of salt spray” without identifying the standard, sample preparation, exposure conditions, or failure definition. |
| Passivation and Cleaning | Use a documented cleaning and passivation process when required by the application or purchase specification. | Parts are free from iron contamination and processing residues after treatment and packaging. | Review the process parameters and perform an agreed free-iron or contamination test on representative samples. ASTM A967 may be referenced for chemical passivation treatments when applicable. | Passivation process record, chemical or bath-control log, and test results. | The supplier claims that stainless steel never needs cleaning or passivation, regardless of forming, machining, or handling conditions. |
| Driving Performance | Define the target substrate, pilot-hole size, driver bit, rotational speed, installation depth, and maximum allowable failures. | Samples install to the specified depth without unacceptable head stripping, shaft breakage, bending, or thread failure. | Run a production-lot driving test using the actual screw and a representative substrate. Record installation torque or failure torque when relevant. | Functional test procedure, raw data, failure photographs, and batch identification. | Testing is performed only by hand or in soft test material that does not represent the intended application. |
| Torque and Torsion Behavior | Set a product-specific minimum installation or torsional requirement because values depend on diameter, geometry, grade, and substrate. | The screw withstands the agreed test without head separation, unacceptable recess damage, or shaft fracture before the specified limit. | Use calibrated torque equipment and a documented fixture. Do not apply a generic torque value unless it has been technically validated for the exact screw. | Torque or torsion test report, equipment calibration certificate, and test-fixture description. | The supplier provides a torque number without test conditions or uses a value copied from a different screw size. |
| Manufacturing Process Control | Control wire or bar receipt, heading, thread forming, point forming, heat treatment if applicable, cleaning, passivation, sorting, and packing. | Each process has defined parameters, inspection points, responsible personnel, and records for the production lot. | Conduct a process audit and review work instructions, control plans, nonconformance records, and corrective-action history. | Process flow chart, control plan, inspection instructions, and batch production record. | Critical operations are subcontracted without disclosure or no records exist for forming, cleaning, or sorting. |
| Sampling and Final Inspection | Use a documented sampling plan based on lot size and risk. Critical safety or fit characteristics may require tightened inspection or 100% sorting. | The inspection level, acceptance number, defect classification, and sample quantity are agreed before shipment. | Apply a recognized sampling approach such as ISO 2859-1 when appropriate, while defining stricter requirements for critical characteristics. | Final inspection report containing lot size, sample size, inspection level, results, and disposition. | The report says only “passed” and does not identify the production lot, sample size, or actual measurements. |
| Packaging and Traceability | Protect screws from moisture, contamination, mixing, and mechanical damage during transport and storage. | Packaging identifies size, grade, quantity, production lot, and inspection status. Cartons remain dry and undamaged. | Check packaging materials, labels, quantity accuracy, carton strength, and traceability from shipment back to raw material. | Packing list, carton-label photographs, lot records, and traceability matrix. | Different grades or sizes are mixed, labels are handwritten without lot information, or packaging allows moisture ingress. |
| Pre-Shipment Approval | Approve a production sample or golden sample before mass production and retain reference samples from each shipment. | The shipped product matches the approved sample in material, dimensions, finish, packaging, and driving performance. | Complete a pre-shipment inspection and compare results with the approved drawing, specifications, and reference sample. | Approved sample record, pre-shipment inspection report, photographs, and retained-sample number. | The supplier changes raw material, tooling, surface treatment, or packaging without written notification and approval. |
How to Choose Top Stainless Steel Wood Screws from China?
Supplier verification should begin with evidence, not attractive product photos. Request the company’s legal registration details, factory address, export history, and recent customer references. A video tour is useful, but an independent factory audit is stronger. Check whether the supplier controls cold heading, thread rolling, heat treatment, surface finishing, and packaging internally. Outsourced processes can create quality gaps. Ask for samples from normal production, not specially prepared samples.
Certifications require careful checking. ISO 9001 can indicate a documented quality system, but it does not guarantee perfect screws. Request material test reports for stainless steel grade, hardness, dimensions, and corrosion resistance. Confirm that reports match the actual production batch. Accredited laboratory testing adds credibility. Salt-spray results are helpful, although they cannot represent every outdoor environment. A polished certificate file may still hide weak traceability.
Tips: Compare certificates with issuing-body records. Ask for batch numbers. Inspect thread sharpness and drive recesses. Measure several samples, not one. Production capacity also matters. Request monthly output, equipment numbers, normal lead time, and peak-season capacity. Ask how the supplier handles urgent orders and machine breakdowns. Capacity claims can be inflated. I would verify them through production records, warehouse observations, and a small trial order. One overlooked detail is packaging; loose screws may rub together and damage the coating before delivery.
How to Choose Top Stainless Steel Wood Screws from China?
Pricing should be compared by specification, not by unit cost alone. Stainless steel grade, screw length, thread design, head type, and surface finish affect the final price. A low quotation may exclude tooling, packaging, inspection, or export charges. Ask for a clear breakdown based on your target order quantity. Confirm whether the price is EXW, FOB, CIF, or another delivery term. Each option changes your transport responsibility and landed cost.
Samples matter. Request screws matching the proposed material grade, dimensions, thread profile, and head tolerance. Samples should include packaging details, not only loose pieces. Test them in the actual wood species and with your intended driver. Check insertion resistance, head seating, corrosion appearance, and thread damage. Small differences become costly during installation. I have seen attractive samples fail when production batches used a different coating process. That mistake was avoidable.
Delivery terms need written precision. Confirm sample lead time, production lead time, shipping method, carton quantity, and loading port. Ask how delays, damaged cartons, and short shipments will be handled. A practical purchase order should list inspection timing and acceptable tolerances. Third-party inspection can verify dimensions, material documents, and carton counts before shipment. It adds expense, but sometimes protects a larger investment. Do not rely on “fast delivery” alone. Get dates. Also review payment stages carefully, especially when custom tooling or large quantities are involved.